|
|
| Brand Name: | CHG |
| Model Number: | AC-02 |
| MOQ: | 1 set |
| Price: | 100,000-300,000 USD |
| Payment Terms: | L/C,D/A,D/P,T/T |
| Supply Ability: | 10 sets per year |
Automotive Parts Powder Coating Production Line with Automatic Spraying
CHG designs and supplies automatic powder coating production lines for automotive parts, integrating surface pretreatment, electrostatic powder application, thermal curing, and material handling into a coordinated manufacturing process.
This production line is developed for coating automotive components made from aluminum alloys and steel sheets. It combines elevator-assisted loading, multi-stage chemical pretreatment, controlled drying, automatic powder spraying, manual touch-up, curing, and forced cooling.
The spraying section incorporates stainless steel and PVC spray booths, while temperature and humidity control helps maintain suitable environmental conditions during powder application.
Each production stage is configured according to the customer's workpiece characteristics, required coating performance, production capacity, and factory layout.
The production line consists of several interconnected processing sections designed to support continuous manufacturing operations.
| Production Section | Main Function |
|---|---|
| Elevator-Assisted Loading | Supports workpiece loading and transfer |
| Pre-Degreasing | Removes initial oils and surface contaminants |
| Degreasing | Provides further cleaning of metal surfaces |
| Water Rinsing | Removes residual cleaning chemicals |
| Vitrification Pretreatment | Forms a compatible conversion layer on the metal surface |
| Water Blowing | Removes retained water from workpiece surfaces and recesses |
| Drying Oven | Eliminates residual moisture before spraying |
| Pre-Spraying Cooling | Brings workpieces to suitable powder application conditions |
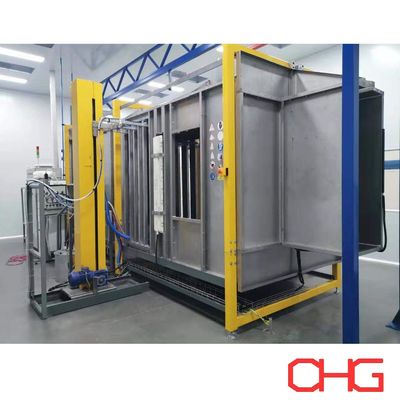
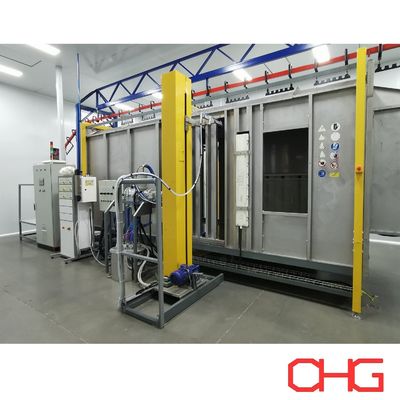
| Stainless Steel and PVC Spray Booths | Provide enclosed powder coating areas |
| Automatic Spray Guns | Perform primary electrostatic powder application |
| Manual Touch-Up Stations | Provide additional coverage where required |
| Temperature and Humidity Control | Maintains specified spraying environment conditions |
| Curing Oven | Thermally cures the powder coating |
| Forced Cooling System | Reduces workpiece temperature after curing |
| Manual Unloading | Allows operators to remove finished components |
The equipment layout and technical parameters are established according to the customer's manufacturing requirements.
Automotive parts may vary significantly in dimensions, material thickness, surface geometry, and coating specifications.
Some components have relatively simple flat surfaces, while others contain stamped sections, welded joints, edges, and recessed areas that require additional consideration during spraying.
This coating line is designed to accommodate different automotive metal products through customized workpiece handling and spraying arrangements.
The system is intended for suitable conductive metal components, including:
Aluminum alloy parts
Steel sheet components
Stamped metal parts
Fabricated automotive assemblies
Welded metal structures
Pretreatment chemistry and powder coating materials must be selected according to the substrate and required performance.
The loading section incorporates lifting equipment to assist with workpiece handling and positioning.
This arrangement can support the transfer of automotive components onto the production line, particularly where product dimensions or handling requirements make direct manual loading less convenient.
The lifting equipment and loading station are engineered according to the workpiece weight, dimensions, hanging arrangement, and required production capacity.
The final loading configuration is coordinated with the conveyor system and workshop layout.
Surface preparation is a critical part of the automotive powder coating process.
Before powder application, metal components must be cleaned and chemically treated to provide suitable conditions for coating adhesion and corrosion resistance.
This production line incorporates a multi-stage pretreatment sequence consisting of pre-degreasing, degreasing, rinsing, vitrification, and water removal.
The initial cleaning stage removes a portion of the oils, lubricants, and other contaminants remaining from stamping, forming, machining, or fabrication.
This reduces the contaminant load entering subsequent treatment stages.
The second cleaning stage provides further removal of processing residues from the metal surfaces.
Cleaning chemistry, temperature, and treatment time are selected according to the substrate and contamination level.
After degreasing, the workpieces pass through rinsing stages to remove residual cleaning chemicals.
Appropriate rinsing helps reduce chemical carryover into the conversion coating stage.
The production line incorporates a vitrification pretreatment process, commonly associated with thin-film conversion coatings used in industrial metal finishing.
Depending on the selected chemical system, this treatment may be suitable for steel and aluminum substrates.
The conversion coating is intended to support powder coating adhesion and corrosion performance.
Pretreatment chemistry and operating parameters must be verified for the actual metal materials and coating specifications.
Following chemical treatment and rinsing, compressed air is used to remove retained water from the workpieces.
This stage is particularly useful for components with folds, channels, recessed sections, or other geometries where water may accumulate.
Water blowing reduces the moisture load entering the drying oven.
After pretreatment, the workpieces enter the drying section.
The drying oven removes remaining moisture before electrostatic powder application.
Drying conditions are determined according to workpiece dimensions, metal thickness, conveyor speed, and the required production capacity.
Following drying, the components pass through a cooling section before entering the spray booth.
This stage helps bring the workpiece temperature within the suitable range for the selected powder coating process.
Controlling workpiece temperature can be important for stable powder deposition and the required surface finish.
The coating application section incorporates spray booths constructed from stainless steel and PVC materials.
The booth arrangement is developed according to the spraying method, workpiece dimensions, powder extraction requirements, and production layout.
Stainless steel construction provides a durable industrial enclosure suitable for specified powder coating operations.
The booth can be designed with appropriate spray gun access, extraction equipment, lighting, and maintenance provisions.
PVC construction offers chemical resistance and facilitates routine cleaning.
The booth dimensions and openings are coordinated with the workpiece envelope and spraying equipment.
The powder application area includes temperature and humidity control to maintain specified operating conditions.
Environmental conditions can affect powder behavior, electrostatic application, and coating consistency.
The required temperature and relative humidity ranges are established according to the powder material, equipment recommendations, and production requirements.
The production line combines automatic powder spraying with supplementary manual application.
This arrangement supports repeatable coating operations while allowing additional attention to complex product geometries.
Automatic electrostatic spray guns apply charged powder particles to grounded automotive components.
The number of spray guns, their positions, and any reciprocating movements are selected according to the workpiece dimensions and coating requirements.
Automatic spraying is particularly suitable for repetitive production involving components with consistent geometries.
Manual spraying stations provide additional application flexibility.
Operators can adjust gun angles and spraying distances to address areas such as:
Welded joints
Recessed surfaces
Stamped corners
Brackets and connecting sections
Complex edges
Areas partially shielded from automatic guns
The need for manual touch-up depends on the actual workpiece geometry and required coating coverage.
After powder application, the coated automotive components enter the curing oven.
During heating, the powder coating melts and flows to form a continuous film. Thermosetting powder coatings subsequently undergo chemical cross-linking to develop their specified properties.
The curing system is designed according to the selected powder manufacturer's requirements.
Important design factors include:
Required metal temperature
Curing residence time
Workpiece material
Metal thickness
Component dimensions
Conveyor speed
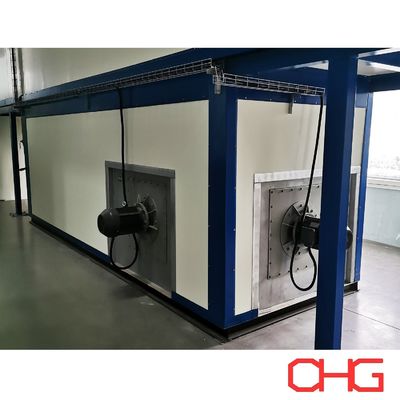
Oven air circulation
Temperature uniformity
Heating energy
Because steel and aluminum components may have different thermal characteristics, the curing arrangement must be evaluated according to the actual products.
Following curing, the coated workpieces enter a forced cooling section.
Air circulation accelerates cooling and helps prepare the components for subsequent handling.
The cooling system is configured according to the workpiece mass, required production throughput, and available factory space.
After cooling, operators manually remove the finished components from the production line.
The products can then proceed to inspection, assembly, packaging, or other manufacturing operations.
The complete process can be summarized as follows:
Elevator-Assisted Loading → Pre-Degreasing → Degreasing → Rinsing → Vitrification Pretreatment → Water Blowing → Drying → Pre-Spraying Cooling → Automatic Powder Spraying → Manual Touch-Up → Curing → Forced Cooling → Manual Unloading
Quality inspection can be incorporated according to the customer's production and quality management requirements.
Automotive components may require specific coating performance standards depending on their application and service environment.
The production line is designed to support controlled processing conditions across the pretreatment, spraying, and curing stages.
Typical quality inspection items include:
Dry film thickness
Surface appearance
Coating adhesion
Color consistency
Gloss level
Coating coverage
Curing performance
Corrosion resistance
Additional tests may be required according to the customer's automotive specifications.
Coating quality depends on the combined performance of substrate preparation, coating materials, application parameters, curing conditions, and production control.
The line can be engineered for suitable aluminum alloy and steel components using compatible pretreatment chemistry and coating materials.
The multi-stage pretreatment system provides cleaning, rinsing, and conversion treatment before powder application.
Temperature and humidity control supports a more stable environment for electrostatic powder coating.
Automatic spray guns handle the primary coating operation, while manual touch-up provides flexibility for complicated automotive components.
Drying, pre-spraying cooling, curing, and forced cooling are integrated into the production sequence.
Elevator-assisted loading and manual unloading can be configured according to the customer's workpiece characteristics and factory conditions.
The equipment is arranged to coordinate the movement of workpieces between processing sections and reduce unnecessary handling.
The powder coating line can be customized for suitable metal components used in automotive manufacturing, including:
Automotive brackets
Steel sheet assemblies
Aluminum alloy components
Vehicle structural supports
Battery enclosure components
Automotive equipment housings
Stamped metal parts
Welded automotive assemblies
Metal reinforcement components
Other fabricated automotive parts
Product suitability depends on the substrate, component geometry, coating specification, and required production capacity.
| Parameter | Configuration |
|---|---|
| Application | Automotive metal components |
| Substrate Materials | Aluminum alloys and steel sheets |
| Loading | Elevator-assisted |
| Unloading | Manual |
| Pretreatment | Pre-degreasing, degreasing, rinsing, and vitrification |
| Water Removal | Compressed-air blowing |
| Drying | Integrated drying oven |
| Pre-Spraying Cooling | Included |
| Spray Booth Materials | Stainless steel and PVC |
| Powder Application | Automatic spraying with manual touch-up |
| Spraying Environment | Temperature and humidity controlled |
| Curing | Integrated thermal curing |
| Post-Curing Cooling | Forced cooling |
| Production Capacity | Customized |
| Workpiece Dimensions | According to product specifications |
| Automation Level | Project-specific |
| Factory Layout | Customized |
CHG develops automotive powder coating production lines according to the customer's actual manufacturing requirements.
To prepare a preliminary design and quotation, please provide:
Automotive component drawings or photographs
Workpiece materials
Maximum length, width, and height
Maximum individual workpiece weight
Required hourly or daily production capacity
Required coating thickness
Powder coating specifications
Corrosion resistance requirements
Pretreatment specifications
Number of coating colors
Color-change frequency
Available factory dimensions
Workshop clear height
Heating energy and electrical supply
Applicable automotive quality standards
Required automation level
Based on these parameters, CHG can develop a technical proposal covering the pretreatment system, loading equipment, spray booths, automatic and manual spraying equipment, drying and curing ovens, cooling sections, material handling, and overall production line controls.
CHG provides complete powder coating production line solutions for manufacturers requiring integrated surface finishing equipment for automotive metal parts.
This configuration combines multi-stage vitrification pretreatment, elevator-assisted loading, stainless steel and PVC spray booths, automatic spraying with manual touch-up, controlled spraying conditions, thermal curing, and forced cooling.
The system is engineered according to the customer's component materials, production capacity, coating requirements, and factory layout.
Contact CHG with your automotive part specifications and manufacturing requirements to receive a customized powder coating production line proposal and quotation.
![]()
![]()