logo

products details

Created with Pixso. Home Created with Pixso. Products Created with Pixso.
Powder Coating Line
Created with Pixso.

Metal Shelves Powder Coating Production Line with Power Free Conveyor System

Metal Shelves Powder Coating Production Line with Power Free Conveyor System

Brand Name: CHG
Model Number: AC-32
MOQ: 1 set
Price: 100,000-300,000 USD
Payment Terms: L/C,D/A,T/T,D/P
Supply Ability: 10 sets per year
Detail Information
Place of Origin:
China
Certification:
CE, ISO
Model NO.:
AC-32
Method Type:
Automatic
Control Unit:
PLC
Mini Order Qty:
1 Set
Size:
Customized
Technical Data:
Customized
Transport Package:
Customized
Packaging Details:
Varies depending on the design
Highlight:

Metal Shelves Powder Coating Line

,

Powder Coating Line Power Free Conveyor

,

Powder Coating Production Line System

Product Description

Heavy-Duty Powder Coating Line for Industrial Shelving and Long Metal Components

Customized Powder Coating System with 13.5-Meter Workpiece Capacity

CHG provides custom-engineered powder coating production lines for industrial shelving, warehouse storage systems, and oversized metal components requiring specialized material handling and surface finishing equipment.

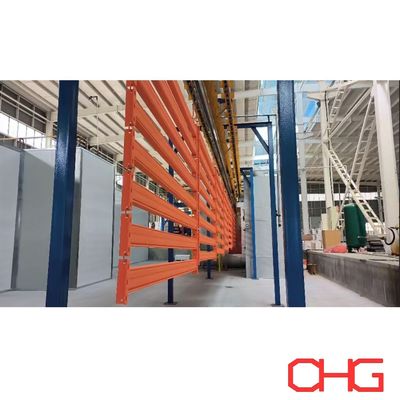
This production line is designed to accommodate suspended workpieces with a maximum hanging length of 13.5 meters. It integrates a polypropylene (PP) powder spray booth, automatic electrostatic spraying equipment, manual touch-up stations, and a heavy-duty Power and Free conveyor.

The system is developed to handle long shelving components while maintaining suitable workpiece positioning throughout surface preparation, powder application, and curing.

By combining automatic coating equipment with flexible manual operations, the production line can accommodate different shelving structures, support profiles, and fabricated metal components.

Main Equipment Specifications

Item Configuration
Application Industrial shelving and warehouse storage components
Maximum Hanging Length 13.5 meters
Spray Booth Material Polypropylene (PP)
Powder Application Automatic electrostatic spraying with manual touch-up
Conveyor System Power and Free overhead conveyor
Carrier Design Reinforced, customized for long workpieces
Loading Method Manual
Unloading Method Manual
Pretreatment High-pressure cleaning and chemical conversion treatment
Conversion Coating Zinc phosphating for suitable steel substrates
Curing System Extended-length curing oven
Temperature Control Zoned heating configuration
Production Capacity Customized
Factory Layout Project-specific engineering

The final equipment dimensions, conveyor arrangement, and operating parameters are determined according to the actual shelving products and required production output.

Specialized Design for Long Shelving Components

Industrial shelving systems often include elongated steel profiles, beams, uprights, brackets, and structural support members.

These components may vary considerably in length, cross-sectional geometry, and weight.

Processing long workpieces requires careful coordination between the conveyor, spray booth, curing oven, and loading stations.

For this project, the coating line is designed around a maximum suspended workpiece length of 13.5 meters.

Engineering Considerations

Important design factors include:

  • Maximum workpiece length and width

  • Hanging orientation

  • Workpiece weight and center of gravity

  • Carrier spacing

  • Conveyor track clearance

  • Spray gun positioning

  • Booth opening dimensions

  • Curing oven clearance

  • Loading and unloading accessibility

  • Required production throughput

The hanging arrangement is designed to maintain suitable workpiece stability during transportation and coating.

Polypropylene Powder Spray Booth

The production line features a PP powder coating booth configured for oversized shelving components.

Polypropylene offers corrosion resistance and a surface suitable for routine cleaning in industrial powder coating environments.

The booth is designed with an extended application area to accommodate long suspended products and the required spray gun arrangement.

Spray Booth Configuration

Depending on the product geometry and production requirements, the booth can incorporate:

  • Automatic electrostatic spray guns

  • Reciprocating spray equipment

  • Manual touch-up positions

  • Powder extraction equipment

  • Powder recovery connections

  • Suitable lighting

  • Cleaning and maintenance access

  • Customized conveyor openings

The spraying area is arranged according to the actual workpiece envelope and required coating coverage.

For long metal components, gun positioning and conveyor movement must be coordinated to provide suitable application conditions along the entire product length.

Automatic Powder Spraying with Manual Touch-Up

The coating system combines automatic electrostatic application with supplementary manual spraying.

Automatic Electrostatic Spraying

Automatic spray guns perform the primary powder application as shelving components travel through the spray booth.

Gun quantity, positioning, reciprocator movement, and powder delivery parameters are selected according to the product dimensions and required coating thickness.

For regularly shaped shelving profiles, automatic spraying can provide repeatable application sequences and reduce the need for continuous manual coating.

Manual Coating Stations

Industrial shelving components may contain brackets, joints, recessed areas, and complicated structural features.

Manual touch-up stations allow operators to provide additional coating coverage where required.

Operators can adjust the spray gun angle and application distance to accommodate different product geometries.

This combined arrangement is useful for production involving both standard shelving profiles and customized structural components.

Coating Long Components Without Workpiece Rotation

The spraying arrangement is designed to coat suspended shelving components without requiring them to rotate during powder application.

Instead, suitable spray gun positioning and application directions are selected according to the workpiece geometry.

This can simplify the workpiece handling arrangement by avoiding a dedicated rotation mechanism.

However, coating accessibility must be evaluated for each product design, particularly where profiles contain deep recesses, overlapping surfaces, or partially enclosed sections.

Additional spray guns or manual touch-up may be required to achieve the specified coverage.

Power and Free Conveyor for Heavy-Duty Material Handling

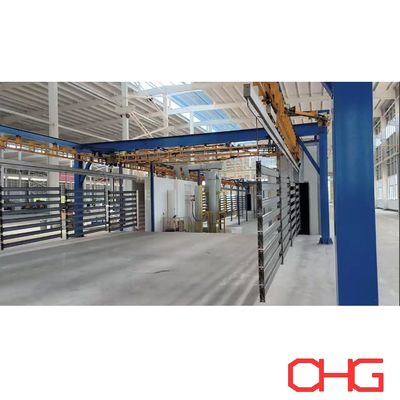
The production line incorporates a Power and Free conveyor designed to transport long metal components between processing stations.

The conveyor uses separate power and free tracks, allowing carriers to stop, accumulate, and resume movement at designated positions.

This provides greater flexibility than a conventional continuously driven conveyor, particularly where loading, spraying, and curing operations require different handling arrangements.

Reinforced Carrier System

Customized carriers are developed to support the long shelving components.

Carrier engineering considers:

  • Workpiece dimensions

  • Total suspended weight

  • Center of gravity

  • Required hanging orientation

  • Number of components per carrier

  • Track clearance

  • Movement stability

  • Loading and unloading requirements

The conveyor load capacity is calculated according to the actual products and supporting fixtures.

Controlled Production Flow

The Power and Free conveyor can support:

  • Carrier accumulation before processing sections

  • Controlled movement through coating areas

  • Independent stopping at designated stations

  • Coordination with loading and unloading operations

  • Flexible carrier release

  • Integration with production line controls

The track layout is developed according to the available factory dimensions and the required material flow.

Surface Preparation for Industrial Shelving

Proper surface preparation is important for achieving the required coating adhesion and corrosion resistance.

For steel shelving components, the pretreatment system can incorporate cleaning, degreasing, rinsing, and zinc phosphate conversion treatment.

The exact chemical process is selected according to the substrate, initial surface condition, and coating specification.

High-Pressure Cleaning

High-pressure spray cleaning can be used to remove surface contaminants from shelving profiles and fabricated steel components.

Spray nozzle arrangement, pressure, and treatment time are selected according to the workpiece geometry and cleaning requirements.

Special attention may be required for channels, corners, and other areas where contaminants can accumulate.

Chemical Degreasing

Degreasing removes oils, grease, and processing residues generated during metal fabrication.

The cleaning chemistry and operating conditions are selected according to the contamination level and required surface preparation quality.

Zinc Phosphate Pretreatment

For suitable steel substrates, zinc phosphating can provide a conversion layer that supports coating adhesion and corrosion resistance.

The pretreatment process may include multiple cleaning, rinsing, conditioning, and phosphating stages.

Chemical parameters and treatment conditions are established according to the selected pretreatment system.

Powder Coating Production Process

A typical process arrangement includes:

Manual Loading → Surface Cleaning → Chemical Pretreatment → Drying → Automatic Powder Spraying → Manual Touch-Up → Curing → Cooling → Inspection → Manual Unloading

1. Loading

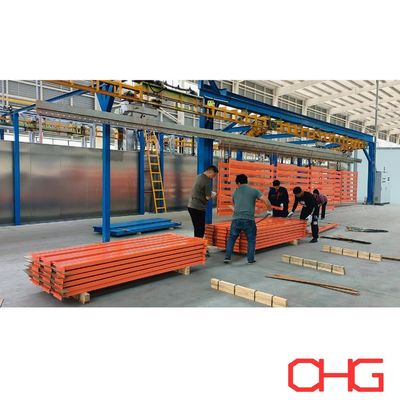
Operators position shelving components onto customized conveyor carriers.

The hanging arrangement is selected according to product length, weight, and required coating accessibility.

2. Surface Treatment

The suspended workpieces undergo cleaning and chemical pretreatment to prepare the metal surfaces for powder coating.

The process is configured according to the required coating performance.

3. Moisture Drying

After pretreatment, the workpieces pass through a drying oven to remove residual surface moisture.

Drying conditions are determined according to workpiece dimensions, material thickness, and production requirements.

4. Powder Application

Automatic electrostatic spray guns apply powder to the grounded metal components.

Manual operators provide supplementary coating where necessary, particularly around brackets, connections, and recessed areas.

5. Thermal Curing

After powder application, the workpieces enter the curing oven.

Controlled heating causes the powder to melt and flow. Thermosetting powder coatings then undergo chemical cross-linking to develop their specified properties.

The oven is designed according to the powder manufacturer's curing requirements and the thermal characteristics of the workpieces.

6. Cooling and Inspection

After curing, the coated components enter the cooling area.

Finished shelving parts can be inspected for coating thickness, appearance, adhesion, and other specified quality requirements before unloading.

Extended-Length Curing Oven

Long shelving components require a curing system with sufficient internal clearance and heating capacity.

The oven arrangement is developed according to the workpiece dimensions, hanging orientation, conveyor movement, and required curing residence time.

Zoned Temperature Control

The curing oven can incorporate multiple heating zones to support temperature management along the processing path.

Important design considerations include:

  • Maximum workpiece dimensions

  • Workpiece mass

  • Required metal temperature

  • Powder curing specification

  • Conveyor speed

  • Heating method

  • Air circulation

  • Temperature uniformity

  • Oven insulation

  • Maintenance access

The curing conditions are established according to the actual metal temperature requirements rather than relying solely on the oven air temperature.

Advantages of the Customized Shelving Powder Coating Line

Processing of Oversized Components

The line is designed for suspended workpieces with a maximum length of 13.5 meters, making it suitable for selected long shelving and structural products.

Flexible Powder Application

Automatic spraying handles the primary coating operation, while manual touch-up provides additional flexibility for complicated product geometries.

Controlled Conveyor Transportation

The Power and Free conveyor supports carrier accumulation and independent stopping at designated processing stations.

Customized Workpiece Support

Reinforced carriers and hangers are engineered according to the dimensions and weight distribution of the shelving components.

Integrated Surface Pretreatment

Cleaning and chemical conversion treatment can be incorporated to prepare steel surfaces for powder coating.

Application-Specific Curing

The extended curing oven is designed around long workpieces and the required thermal processing conditions.

Typical Applications

This production line can be adapted for a range of long metal products, including:

  • Industrial shelving systems

  • Warehouse storage racks

  • Heavy-duty shelving uprights

  • Long steel beams

  • Storage system support profiles

  • Metal rack frames

  • Industrial structural members

  • Fabricated steel assemblies

  • Long metal support components

  • Customized warehouse equipment

Product suitability depends on dimensions, weight, hanging arrangement, and coating specifications.

Customized Engineering and Production Capacity

CHG develops each powder coating line according to the customer's actual products and manufacturing requirements.

Design Parameter Engineering Scope
Maximum Workpiece Length Up to 13.5 meters for this configuration
Workpiece Width and Height According to product drawings
Workpiece Weight Determines conveyor and carrier design
Production Capacity Customized
Conveyor Speed Calculated according to required throughput
Carrier Spacing Based on product dimensions and clearance
Spray Booth Extended PP construction
Spray Gun Arrangement Automatic with manual touch-up
Powder Recovery Selected according to operating requirements
Pretreatment Cleaning and zinc phosphating for suitable steel parts
Drying System Integrated with production flow
Curing Oven Extended-length, zoned heating configuration
Cooling Designed according to workpiece requirements
Control System Project-specific
Workshop Layout Customized

Information Required for a Technical Proposal

To develop a suitable powder coating production line, please provide:

  • Shelving component drawings or photographs

  • Maximum product length, width, and height

  • Maximum individual workpiece weight

  • Required hourly or daily production capacity

  • Number of components per hanger

  • Workpiece material

  • Required coating thickness

  • Powder coating specifications

  • Corrosion resistance requirements

  • Number of colors

  • Color-change frequency

  • Available workshop dimensions

  • Factory clear height

  • Heating energy and electrical supply

  • Loading and unloading requirements

Based on these parameters, CHG can prepare a customized equipment layout and technical proposal covering the pretreatment system, Power and Free conveyor, PP powder spray booth, automatic and manual spraying equipment, powder recovery system, curing oven, and production line controls.

Industrial Shelving Powder Coating Solutions from CHG

CHG provides integrated powder coating production line solutions for manufacturers processing oversized metal shelving and long structural components.

This configuration combines a 13.5-meter hanging capacity, polypropylene powder spray booth, automatic spraying with manual touch-up, and a heavy-duty Power and Free conveyor.

The production line is engineered according to the customer's workpiece characteristics, factory conditions, and required production capacity.

Contact CHG with your shelving component drawings, maximum workpiece dimensions, and production requirements to receive a customized powder coating line design and quotation.