logo

products details

Created with Pixso. Home Created with Pixso. Products Created with Pixso.
Liquid Painting Line
Created with Pixso.

Automatic Method Type Coating Production Line for Carbon Steel Parts Professional Liquid Paint Line

Automatic Method Type Coating Production Line for Carbon Steel Parts Professional Liquid Paint Line

Brand Name: CHG
Model Number: AC-04
MOQ: 1 set
Price: 100,000-300,000 USD
Payment Terms: D/P,T/T,D/A,L/C
Supply Ability: 10 sets per year
Detail Information
Place of Origin:
China
Certification:
CE, ISO
Coating:
Painting
Substrate:
Steel
Mini Order Qty:
1 Set
Categories:
Coating Production Line
Control Unit:
PLC
Transport Package:
Customized
Supply Ability:
10/Year
Packaging Details:
Varies depending on the design
Highlight:

Automatic coating production line carbon steel

,

Liquid paint line carbon steel parts

,

Professional liquid painting line automatic

Product Description

Automatic Liquid Dip Coating Line for Heavy Carbon Steel Structural Parts

Customized Industrial Painting System with Power and Free Conveyor
CHG provides custom-engineered liquid dip coating production lines for carbon steel structural components, combining controlled immersion coating, overhead material handling, extended drip-off time, and thermal drying into an integrated production system.
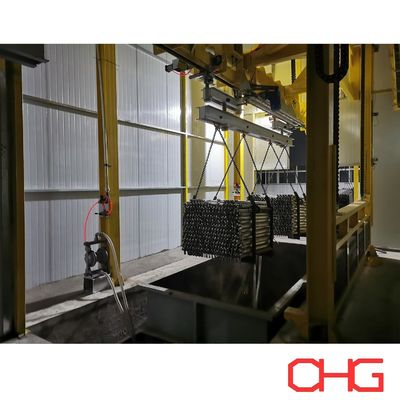
This line features a 45° angled dipping station and a Power and Free conveyor, allowing heavy workpieces to move between different processing stages while accommodating the residence times required for immersion coating, paint drainage, and drying.
The system is designed for structural steel components weighing up to 2,000 kg per carrier, with forklift-assisted manual loading and unloading. Its conveyor speed is adjustable from 0.5 to 3.0 m/min, providing flexibility for different operating conditions.
The equipment arrangement, dipping tank dimensions, carrier design, and production layout can be customized according to the customer's workpieces and coating requirements.

Main Equipment and Technical Configuration

Parameter Specification
Coating Method Liquid immersion / dip coating
Workpiece Material Carbon steel
Dipping Arrangement 45° angled dipping
Conveyor Type Power and Free overhead conveyor
Maximum Carrier Load 2,000 kg
Conveyor Speed Adjustable, 0.5–3.0 m/min
Loading Method Manual, forklift-assisted
Unloading Method Manual, forklift-assisted
Immersion Time 6 minutes
Drip-Off Time 90 minutes
Drying Time 48 minutes
Drying Temperature 60–80°C
Cooling Time 6 minutes
Dipping Tank Dimensions Customized
Equipment Layout Project-specific engineering
The operating parameters above describe this production line configuration. For other projects, coating time, drying conditions, conveyor capacity, and equipment dimensions are determined according to the actual products and coating materials.


45° Angled Immersion Coating System

The dipping section is designed to immerse carbon steel structural components into the liquid coating material at a 45-degree angle.
This arrangement can be useful for products with complex structural features, including welded assemblies, internal corners, and interconnected steel sections.
The angled dipping mechanism is engineered according to the workpiece dimensions, hanging arrangement, center of gravity, and coating requirements.

How the Immersion Process Works

During operation, the workpieces are transported to the dipping station by the overhead conveyor.
The dipping equipment positions the suspended components for immersion into the coating tank.
The workpieces remain immersed for the specified processing period before being withdrawn and transferred to the drip-off section.
For this line, the designed immersion duration is 6 minutes.
The dipping tank and associated mechanisms are configured according to the required workpiece envelope, coating liquid characteristics, and production capacity.

Advantages of Immersion Application

Compared with conventional spray application, immersion coating can provide access to surfaces that may be difficult to reach with spray guns.
Potential advantages include:
  • Coating of complicated structural geometries
  • Application to recessed and partially enclosed surfaces
  • Reduced dependence on manual spray gun positioning
  • Repeatable immersion sequences
  • Integration with automated workpiece transportation
  • Suitability for selected heavy fabricated steel products
Actual coating coverage and film uniformity depend on component geometry, drainage characteristics, paint formulation, immersion conditions, and process control.


Power and Free Conveyor for Heavy-Duty Workpieces

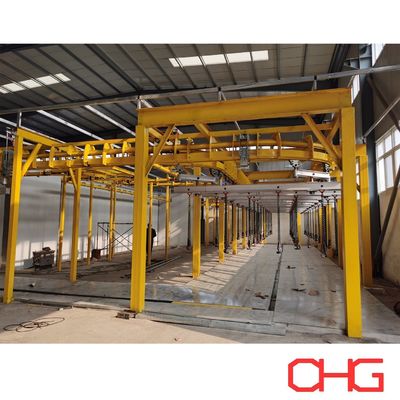
The production line uses a Power and Free overhead conveyor to transport components between loading, dipping, drip-off, drying, cooling, and unloading stations.
Unlike a conventional continuously driven conveyor, a Power and Free system allows carriers to stop, accumulate, and resume movement at designated positions.
This functionality is particularly useful for liquid dip coating processes where different stages require significantly different processing times.

Independent Carrier Movement

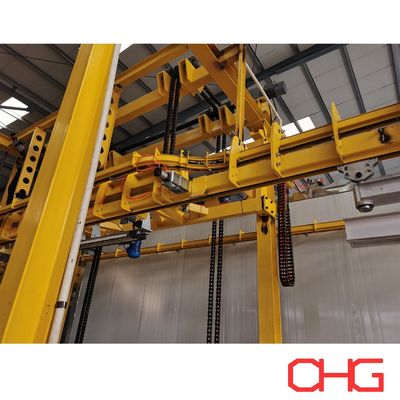
The conveyor incorporates separate power and free tracks.
Individual carriers can be engaged or disengaged from the driving mechanism, allowing controlled movement through the production line.
Depending on the track layout and control arrangement, the system can support:
  • Carrier accumulation
  • Controlled stopping at processing stations
  • Sequential carrier release
  • Coordination of immersion operations
  • Extended residence time in designated areas
  • Flexible movement between production stages

Heavy-Duty Carrier Design

The specified maximum carrying capacity is 2,000 kg per carrier.
Carriers and hangers are designed according to the workpiece weight, dimensions, center of gravity, and suspension requirements.
For heavy structural components, proper load distribution and stable workpiece positioning are important considerations throughout transportation and immersion.

Adjustable Conveyor Speed

The conveyor operating speed can be adjusted within the specified range of 0.5–3.0 m/min.
This provides flexibility for material movement between different sections.
Actual production throughput depends on carrier spacing, workpiece loading quantity, processing time, accumulation capacity, and the overall conveyor layout.


Production Process and Operating Sequence

The production line follows six main operating stages:
Forklift-Assisted Loading → Angled Dip Coating → Drip-Off → Thermal Drying → Natural Cooling → Forklift-Assisted Unloading

Stage 1: Forklift-Assisted Loading

Carbon steel structural components are transported to the loading station using a forklift.
Operators position the workpieces onto the designated carriers or hanging fixtures.
The loading arrangement is designed to accommodate the product dimensions, weight, and required coating orientation.
Once the workpieces are securely positioned, the Power and Free conveyor transfers them toward the dipping station.

Stage 2: Liquid Immersion Coating

Process time: 6 minutes
The workpieces enter the angled dipping station and are immersed in the liquid coating material.
The 45° dipping arrangement is intended to facilitate immersion of the structural components according to their geometry.
Immersion duration and movement sequences are controlled according to the process requirements.
Following the specified dipping period, the coated workpieces are withdrawn from the tank and transferred to the next station.

Stage 3: Paint Drip-Off

Process time: 90 minutes
After immersion, the coated structural parts remain in a designated drip-off area.
This stage allows excess liquid coating material to drain from the workpiece surfaces before thermal drying.
The relatively long drip-off period is an important characteristic of this production line.
The Power and Free conveyor can accommodate the required residence time through suitable accumulation and carrier positioning arrangements.
The drip-off section is designed with consideration for workpiece spacing, drainage direction, coating collection, and available workshop space.

Stage 4: Thermal Drying

Process time: 48 minutes
Drying temperature: 60–80°C
Following the drip-off stage, the coated components enter the drying oven.
Controlled heating removes volatile components and supports the film-forming or curing process required by the selected liquid coating system.
The specified operating conditions for this line are 48 minutes at 60–80°C.
The final drying performance depends on the coating formulation, workpiece thickness, actual metal temperature, airflow, and heating conditions.
Oven design must also account for the safety and ventilation requirements associated with the selected coating materials.

Stage 5: Natural Cooling

Process time: 6 minutes
After drying, the workpieces enter the natural cooling section.
The specified cooling duration is 6 minutes.
During this stage, the temperature of the coated components decreases before unloading and subsequent handling.
Actual unloading temperature depends on workpiece mass, geometry, ambient conditions, and cooling area design.

Stage 6: Forklift-Assisted Unloading

At the final station, finished structural components are removed from the conveyor using forklift-assisted manual handling.
The workpieces can then proceed to inspection, assembly, storage, or subsequent manufacturing operations.
The unloading area is arranged according to the product dimensions, handling method, and available factory space.

Production Flow and Process Timing

Production Stage Operating Time Main Purpose
Loading According to handling requirements Secure workpiece positioning
Angled Dip Coating 6 minutes Liquid coating application
Drip-Off 90 minutes Drainage of excess coating material
Thermal Drying 48 minutes Drying and film formation
Natural Cooling 6 minutes Reduction of workpiece temperature
Unloading According to handling requirements Removal of finished components
The specified immersion, drip-off, drying, and cooling stages total 150 minutes of process residence time, excluding loading, unloading, and transportation delays.
This does not represent the production cycle time per carrier or the interval between finished batches. Actual line throughput depends on the number of carriers that can be processed simultaneously within each section and the complete conveyor arrangement.


Advantages of the Structural Steel Dip Coating Line

Suitable for Heavy Structural Components

The conveyor system is configured for workpieces weighing up to 2,000 kg per carrier, making it suitable for selected medium-to-heavy fabricated steel products.

Controlled Immersion Coating

The angled dipping station provides a defined coating application process that can be adapted to complex structural geometries.

Extended Drip-Off Capability

The production line incorporates a dedicated 90-minute drainage stage, allowing excess coating material to drain before the drying process.

Flexible Carrier Management

The Power and Free conveyor supports controlled carrier movement and accumulation, helping coordinate processing stages with different residence times.

Reduced Manual Transportation

Forklifts are used at the loading and unloading stations, while the conveyor handles workpiece movement between the main coating processes.

Customized Equipment Arrangement

Dipping tank dimensions, carrier configuration, conveyor routing, drying equipment, and factory layout can be developed according to the customer's products and production requirements.


Typical Applications

This type of liquid immersion coating system can be considered for suitable carbon steel products such as:
  • Fabricated structural steel assemblies
  • Industrial machinery frames
  • Heavy steel supports
  • Welded metal structures
  • Agricultural equipment components
  • Industrial brackets and frames
  • Construction-related steel components
  • Other fabricated carbon steel products
Product suitability should be evaluated according to geometry, drainage characteristics, coating requirements, and workpiece weight.


Customized Engineering for Liquid Painting Production Lines

CHG develops liquid coating production systems according to the customer's manufacturing process and technical requirements.
Important information for preliminary engineering includes:
  • Workpiece drawings and photographs
  • Carbon steel material specifications
  • Maximum dimensions
  • Maximum individual weight
  • Workpiece center of gravity
  • Required production capacity
  • Number of workpieces per carrier
  • Coating material and technical data
  • Required film thickness
  • Surface preparation requirements
  • Immersion and drainage requirements
  • Drying temperature and time
  • Available factory dimensions
  • Workshop clear height
  • Heating energy
  • Local electrical specifications
  • Loading and unloading conditions
Based on these parameters, the engineering team can determine the appropriate dipping tank, lifting or positioning mechanism, Power and Free conveyor, carrier design, drip-off area, drying oven, cooling section, and control arrangement.


Industrial Liquid Dip Coating Solutions from CHG

CHG provides customized liquid painting production line solutions for industrial manufacturers requiring integrated coating equipment and material handling systems.
This structural steel dipping line combines 45° angled immersion coating, a heavy-duty Power and Free conveyor, forklift-assisted loading and unloading, extended paint drainage, and controlled thermal drying.
The equipment is engineered to accommodate the actual workpiece dimensions, coating process, and required production output.
Contact CHG with your structural component drawings, maximum workpiece weight, coating specifications, and production requirements to receive a customized liquid dip coating line proposal and quotation.