|
|
| Brand Name: | CHG |
| Model Number: | CS-06 |
| MOQ: | 1 set |
| Price: | 5,000-100,000 USD |
| Payment Terms: | D/A,D/P,T/T,L/C |
| Supply Ability: | 50 sets per year |
Flexible Automated Coating System for Industrial Metal Products
This powder coating production line with Power and Free conveyor is designed for manufacturers requiring flexible material handling, controlled production flow, and reliable powder coating performance.
The Power and Free overhead conveyor allows individual carriers to be stopped, accumulated, released, or transferred according to the requirements of different process stages. Compared with a conventional continuous conveyor, this configuration provides greater flexibility when products require different processing times or when multiple workpiece types are handled on the same production line.
The complete coating system can be customized according to the customer's workpiece dimensions, weight, production capacity, coating requirements, factory layout, and required automation level.
Main Production Line Configuration
Depending on the project requirements, a complete Power and Free powder coating line can integrate:
Surface pretreatment system
Moisture drying section
Power and Free overhead conveyor
Automatic powder spray booth
Automatic electrostatic spray guns
Manual touch-up stations
Powder supply and recovery equipment
Powder curing oven
Cooling section
Loading and unloading stations
PLC and HMI control system
Equipment configuration is selected according to the actual coating process rather than using a fixed standard arrangement.
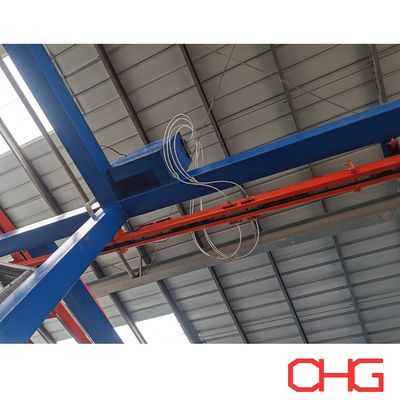
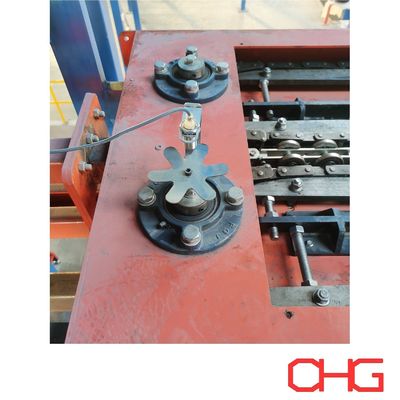
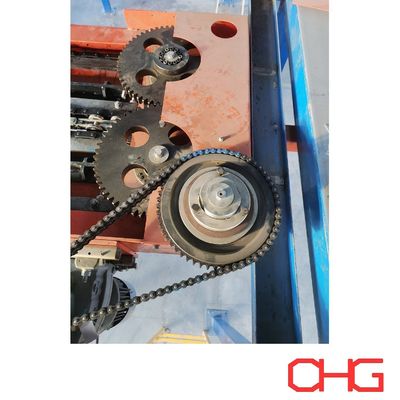
Power and Free Overhead Conveyor
The Power and Free conveyor uses separate power and free tracks.
The power track contains the driven chain, while carriers travel along the free track. Through appropriate engagement and release mechanisms, individual carriers can operate independently within the overall conveyor system.
This allows workpieces to:
Move between different production stages
Stop at designated process positions
Accumulate in buffer areas
Be released according to production requirements
Transfer between conveyor sections
Follow different routes where the process requires
This flexibility is particularly useful in automated coating lines where pretreatment, spraying, curing, cooling, and loading operations may require different process times.
Flexible Carrier and Hanger Design
Carriers and hangers are engineered according to the products being coated rather than using one universal design.
Important factors include:
Maximum workpiece dimensions
Workpiece weight
Number of products per carrier
Hanging orientation
Center of gravity
Required carrier spacing
Spray gun accessibility
Oven opening dimensions
Loading and unloading method
The system can accommodate different carrier configurations ranging from smaller industrial components to large and heavy fabricated metal products.
Automatic Powder Coating Process
A typical production sequence can be configured as:
Loading → Pretreatment → Moisture Drying → Powder Spraying → Powder Curing → Cooling → Inspection → Unloading
1. Loading
Metal components are mounted onto suitable hangers or carriers at the loading station.
Loading can be manual, forklift-assisted, or integrated with other material handling equipment depending on workpiece size and weight.
2. Surface Pretreatment
Before powder application, workpieces undergo the required cleaning and chemical pretreatment process.
Depending on the substrate and coating requirements, the process may include:
Degreasing
Water rinsing
Surface conditioning
Phosphating or other conversion treatment
Final rinsing
Both spray and immersion pretreatment configurations can be considered according to product geometry and production requirements.
3. Moisture Drying
Following wet pretreatment, workpieces pass through a drying section to remove residual moisture before powder application.
Dry and properly prepared surfaces help provide stable electrostatic spraying conditions and reduce coating defects.
4. Electrostatic Powder Spraying
The workpieces enter the powder spray booth, where electrostatic spray guns apply powder to the grounded metal surfaces.
Depending on the required automation level, the spraying section can incorporate:
Automatic spray guns
Reciprocators
Manual touch-up guns
Powder supply equipment
Powder recovery equipment
Automatic spraying provides repeatable application on the main surfaces, while manual touch-up can be used for complex geometries, recessed areas, corners, and other difficult-to-coat locations.
5. Powder Curing
After powder application, carriers transport the coated workpieces into the curing oven.
Under controlled heating conditions, the powder melts, flows, and chemically cross-links to form a continuous coating film.
Curing conditions are determined according to the powder specification, workpiece material, metal thickness, and required coating performance.
6. Cooling
After curing, workpieces move into the cooling area before inspection and unloading.
Natural or forced-air cooling can be selected according to production capacity and available factory space.
7. Inspection and Unloading
Finished products are inspected according to the required coating specification before being removed from the conveyor.
Typical inspection items may include coating thickness, appearance, color, gloss, adhesion, and visible surface defects.
Carrier Accumulation and Production Buffering
One of the major advantages of a Power and Free system is the ability to create accumulation zones within the production line.
Carriers can wait at designated positions without stopping the complete conveyor system.
Buffer areas can be incorporated:
Before spray booths
Before curing ovens
At loading stations
At unloading stations
Between processes with different cycle times
At inspection or production waiting areas
This helps coordinate different production stages and provides greater flexibility when temporary interruptions occur in one section of the line.
Flexible Conveyor Routing
For production lines handling different product types or process requirements, the conveyor can be designed with transfer and routing functions.
Depending on the layout, this can allow certain carriers to:
Enter different coating sections
Bypass selected process areas
Move into accumulation zones
Transfer to alternative production routes
Reach different loading or unloading stations
The actual routing arrangement is determined according to the customer's production process and workshop layout.
PLC-Based Conveyor and Process Control
The Power and Free conveyor can be integrated with the control system of the complete powder coating line.
Depending on the project, the PLC and HMI system can coordinate:
Conveyor operation
Carrier movement
Stop and release positions
Accumulation zones
Conveyor speed
Workpiece detection
Process routing
Equipment interlocking
Spray equipment operation
Oven operation
Fault alarms and status monitoring
This integration allows material handling and coating equipment to operate as a coordinated production system.
Safety and Equipment Protection
Appropriate safety measures can be incorporated according to the conveyor layout, workpiece characteristics, and operating environment.
These may include:
Emergency stop devices
Carrier position detection
Conveyor overload protection
Equipment interlocks
Mechanical guarding
Fault alarms
Anti-collision control where required
Operator protection at loading and unloading areas
Safety configuration is determined during detailed engineering according to the actual production line.
Main Advantages
Flexible Workpiece Transportation
Individual carrier control makes it possible to coordinate workpieces with different process times and production sequences.
Efficient Production Flow
Accumulation and controlled carrier release help balance material movement between different sections of the coating line.
Reduced Manual Handling
Once loaded onto the carriers, workpieces can be automatically transported through multiple coating processes.
Efficient Use of Workshop Space
The overhead conveyor arrangement leaves more floor space available for process equipment, operators, maintenance, and material handling.
Suitable for Different Products
Customized carriers, hangers, spacing, and routing make the system suitable for a wide range of metal components.
Expandable Automation
The conveyor can be integrated with automatic spraying equipment, process control systems, and other production equipment according to the required automation level.
Typical Applications
Power and Free powder coating lines can be engineered for products such as:
Automotive components
Electrical cabinets and enclosures
HVAC products
Metal furniture
Storage racks and shelving
Machinery components
Agricultural equipment
Metal doors and frames
Fabricated steel products
General industrial metal components
Customized Power and Free Powder Coating Lines
Each production line is engineered around the customer's actual manufacturing requirements.
Key information required for system design includes:
Workpiece material
Maximum dimensions
Maximum weight
Products per carrier
Required production capacity
Coating specification
Pretreatment requirements
Number of colors and color-change frequency
Factory dimensions and clear height
Available heating energy
Loading and unloading requirements
Required accumulation positions
Automation level
Based on these parameters, we can develop a customized solution covering the Power and Free conveyor, carrier and hanger system, pretreatment equipment, powder spray booth, powder application and recovery equipment, curing system, cooling section, control system, and complete production line layout.
Contact us with your workpiece information and production requirements for a customized Power and Free powder coating line proposal and quotation.
![]()